Every manufacturer in the food industry is familiar with high humidity in production areas, particularly after cleaning all equipment in a production area. Moisture remains in the air, on walls, and on surfaces, forcing production to be put on hold. In many production environments, this required drying time is an often-underestimated factor that limits the availability of production lines. After all, every extra hour of waiting represents costly, unused production capacity.
Air Quality Process (AQP) has developed an integrated solution for hygienic air handling to optimize this critical phase. Based on a comprehensive airflow analysis, a comprehensive solution is implemented that combines various techniques:
- Controlled airflow within the production area
- Overpressure control to limit unwanted airflow and contamination
- Hygienic air handling for optimal temperature control
- Highly efficient dehumidification of the air during and after the cleaning process.
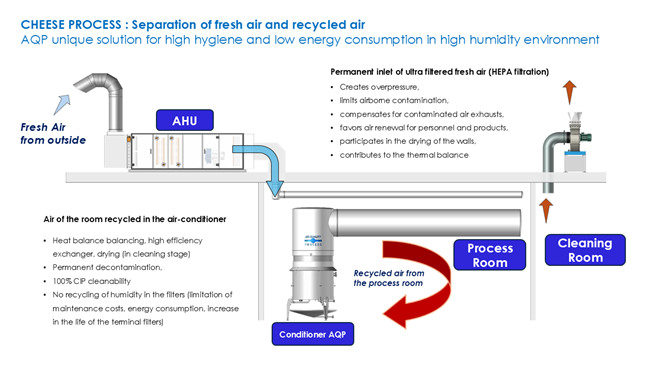
The goal is clear: to remove excess moisture as quickly as possible so that production can resume safely and efficiently. A continuous supply of HEPA-filtered fresh air, combined with controlled air circulation, helps minimize the risk of airborne contamination. At the same time, the drying process for both the room and its surfaces is significantly accelerated. The moisture removed from the ambient air is collected as condensate and discharged. This makes the dehumidification process visible and measurable (see video). For manufacturers in the food industry, this approach offers significant advantages:
- Less condensation in production areas
- Shorter drying times and surfaces that remain wet for a shorter period of time
- Faster resumption of production after cleaning
- Minimize the risk of mold growth and microbial development
- Improved process reliability and hygiene control
With more than 5,000 air conditioners now in operation worldwide and over 30 years of experience in hygienic air treatment, Air Quality Process helps cheese producers improve food safety, product quality, and operational efficiency.
Click here for more information about our hygienic and energy-efficient solutions